Key Takeaways
The right manufacturing system depends on matching it to your most urgent operational and business needs.
- Use ERP to coordinate finance, purchasing, inventory, sales, and long-term material and capacity planning across the business.
- Choose MES for real-time shop-floor control, including machine data, job dispatch, in-process quality, downtime, scrap, and traceability.
- Start with ERP manufacturing features for simple operations; add a dedicated MES when complexity, compliance, genealogy, or machine integration demands it.
- Integrate ERP and MES to connect orders and bills of materials with real-time consumption, WIP, scrap, completion, inventory, and costing data.
- Validate the investment through a pilot, measuring OTIF, lead time, OEE, downtime, scrap, rework, and schedule adherence against baseline performance.
MES or ERP? For many manufacturers, it’s a genuinely confusing decision. Both systems improve efficiency and support better decision-making—but they do it in very different ways. An MES focuses on real-time shop floor operations, tracking production processes as raw materials transform into finished goods. ERP software, on the other hand, manages resources across your entire business, from accounting and inventory to sales and human resources.
What makes this more complex is that MES and ERP integration is often just as important as understanding each system individually. And the choice between them isn’t always either-or. This guide will help you determine which system your manufacturing business actually needs—whether that’s an ERP with built-in MES features, a dedicated MES and ERP combination, or something in between.
What Are MES and ERP Systems?
MES and ERP each occupy a distinct layer of your manufacturing operation. Understanding what each one does—before comparing them—makes it much easier to determine which one your business actually needs.
MES Software: Managing Work on the Shop Floor
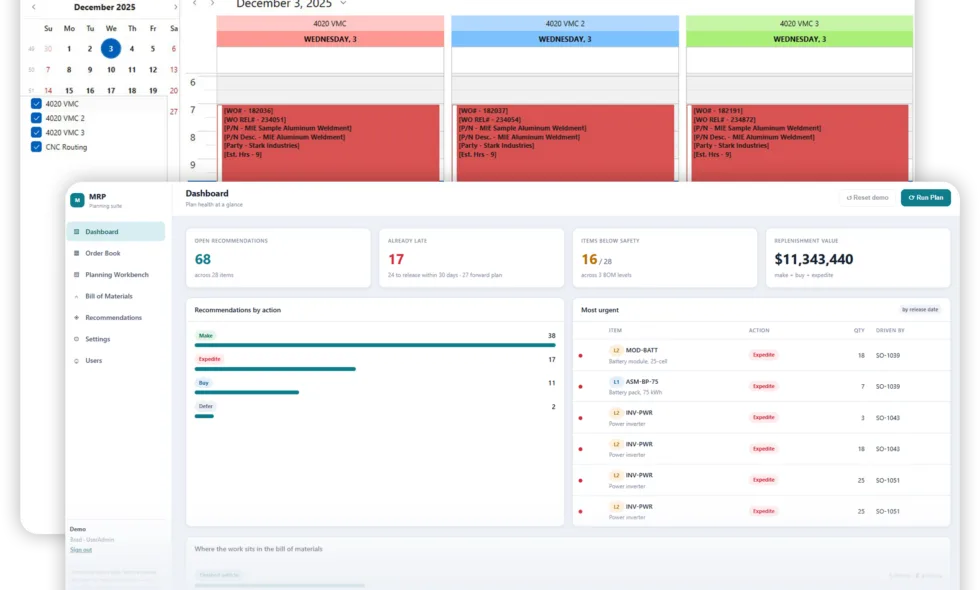
A manufacturing execution system monitors, tracks, documents, and controls the process of manufacturing goods from raw materials to finished products. Sitting between your enterprise planning systems and your process control equipment, an MES gives you the data needed to make your plant floor more efficient.
The Manufacturing Enterprise Solutions Association International identified 11 core MES functions back in 1997—and they remain just as relevant today:
- Resource allocation and status
- Operations scheduling
- Dispatching production units
- Document control
- Data collection and acquisition
- Labor management
- Quality management
- Process management
- Maintenance management
- Product tracking and genealogy
- Performance analysis
Together, these functions track worker schedules, qualifications, cycle times, run states, scrap rates, and machine data—all in real time.
The ISA-95 standard places MES at level three of the manufacturing hierarchy, sitting between business planning at level four and process control systems at levels zero through two. That positioning is what makes MES and ERP integration possible—the two systems can exchange production orders, work instructions, and material usage data across these defined layers.
ERP Software: Managing Resources Across the Business
ERP operates at level four of the ISA-95 hierarchy, handling business planning and logistics. Its focus is on creating and managing plant schedules—covering production, material use, delivery, and shipping—while gathering and organizing information across your entire business.
ERP systems determine what products to manufacture based on finance, procurement, supply chain management, and inventory data. Think of it as the system that connects every facet of your enterprise into a single information system, giving you a clear view of how your business operations perform and interact with one another.
Where MES answers the question “What is happening on the shop floor right now?”, ERP answers “What does the business need to do, and do we have the resources to do it?”
MES vs ERP: Production Control, Data, and Daily Use
The clearest way to tell these two systems apart? Watch what each one does during a single production shift.
Scheduling: Shop-Floor Job Dispatch vs Material and Capacity Planning
MES handles production scheduling at the workstation level—dispatching work orders to specific machines based on current equipment status and material availability. ERP operates at a higher level, calculating what materials are needed, in what quantities, and when. It automatically generates purchase suggestions and work order recommendations based on sales orders, production orders, current inventory levels, and demand forecasts.
Put simply: MES tells your operators what to run next. ERP tells your planners what to order and when.
Data Capture: Machine Signals and Barcodes vs Business Transactions
An MES system uses sensors—sometimes thousands of them—alongside barcode scanners to pull real-time data directly from the production floor. Temperatures, pressures, cycle times, sensor readings: MES captures values that change second by second during active production.
ERP works with a different class of data entirely. Purchase orders, invoices, inventory movements, sales orders—these are the business transactions ERP collects and makes available for operational and financial analysis.
Quality: Process Checks and Product Traceability vs Supplier and Inventory Records
MES monitors machine process controls continuously, storing every change in pressure, flow, and torque value for reporting and analysis. For manufacturers operating in highly regulated industries, MES software also provides part traceability and full genealogy of components—something spreadsheets simply cannot deliver.
ERP, on the other hand, maintains quality records at the supplier and inventory level, tying quality data to costs and financial reporting.
Reporting: Downtime, Scrap, and OEE vs Costs, Cash Flow, and Orders
- MES delivers Overall Equipment Effectiveness (OEE) reporting, downtime tracking, and real-time defect flags.
- ERP generates purchase suggestions, production schedules, and financial reports that can span hours to months.
One system keeps your plant running efficiently today. The other helps you plan for next quarter.
Primary Users: Operators and Plant Managers vs Planners and Finance Teams
MES is built for the people closest to production—operators, process engineers, and plant managers making decisions based on what is happening on the floor right now. ERP serves a broader audience: finance teams, procurement managers, operations executives, and sales staff who need visibility across the entire organization.
MES and ERP Integration: Connecting Production to Business Plans
Think of MES and ERP as two halves of the same operation. One runs the shop floor. The other runs the business. A bidirectional data exchange between the two connects what’s happening at the machine level to what’s being planned in the boardroom. Following the ISA-95 standard, ERP at level four communicates with MES at level three — establishing a structured interface between enterprise planning and production control.
ERP to MES: Production Orders, Bills of Materials, and Work Instructions
ERP sends production-related data downstream to MES as input for coordinating shop-floor operations. This includes production orders, bills of materials, standard operating procedures, change orders, master data, reference product information, and production demand.
Once received, the MES regroups this information to drive manufacturing decisions:
- Which plant or production line to assign the job to
- Which operators have the qualifications and availability to run specific production tasks
- Where to deliver raw materials along the production line
MES to ERP: Material Use, Work in Progress, and Finished Goods
Data flows in the other direction too. MES sends upstream information back to ERP, giving the business layer an accurate, real-time picture of what’s actually happening on the floor. Specifically, MES shares:
- Material consumption, scrap, and completion data — to keep costing and inventory accurate
- Resource usage data covering labor, equipment, and materials
- Order and work-in-progress status, as-built genealogy yields, time events, and machine throughput
As products are completed, MES notifies ERP to immediately deduct used raw materials from inventory and add finished goods to warehouse stock — through real-time backflushing. The result is inventory data you can actually trust.
Built-In MES Features vs a Separate MES: Data Ownership and Connection Needs
Not every manufacturer needs a standalone MES. For simpler operations, ERP’s built-in manufacturing features may be enough. But when production complexity grows — and the gap between what ERP can see and what’s actually happening on the floor widens — a dedicated MES becomes the smarter path.
Companies that successfully integrate their MES and ERP systems see real, measurable gains: increased overall equipment efficiency, reduced cycle times, less manual data entry, greater data consistency, leaner manufacturing, and more on-time delivery. The key word is “successfully” — the quality of the integration matters as much as the decision to integrate.
Which System Does Your Manufacturing Business Need?
The right system isn’t always obvious. What matters most is identifying where your operation is breaking down and what business outcomes need to improve first.
Choose ERP First When Finance, Purchasing, and Orders Need Coordination
Start by building a cross-functional selection committee that includes operations, quality, supply chain, finance, and IT — with executive sponsorship behind it. Before anyone looks at a product demo, anchor the decision in outcomes: what specific improvements do you need in throughput, lead time, inventory turns, and cash conversion? Define those first. Evaluating software screens before defining the problem is how poor decisions get made.
Use ERP Manufacturing Features When They Meet Your Shop-Floor Needs
Not every manufacturer needs a dedicated MES. Simple discrete plants with short routings can often run on an ERP’s built-in manufacturing module alone. The key is to verify — not assume — that production planning, finite capacity scheduling, and mobile data capture actually meet your execution needs without heavy customization. If they do, a separate MES may be an unnecessary investment.
Add a Dedicated MES When Production Complexity or Compliance Demands More
Some environments require more than ERP’s manufacturing features can provide. Manufacturers that need real-time machine integration, strict lot or serial genealogy, in-process quality checks, or regulatory documentation for standards like FDA, AS9100, or IATF 16949 typically require a dedicated MES on the shop floor, integrated with ERP for the business layer. The shop floor drives that decision — not the software catalog.
Compare Total Cost: Licenses, Hardware, Integration, Training, and Support
First-year investment can range from around $50,000 for a small cloud deployment to several million dollars for a large, complex enterprise rollout. That range is wide — and the number that matters is your total cost of ownership over three to seven years. Build a TCO model that accounts for licenses, implementation, integrations, data migration, testing, training, and ongoing support. The sticker price rarely tells the full story.
Check User Reviews for Reliability, Operator Usability, and Vendor Support
One factor that often gets underweighted: the implementation partner frequently matters more than the software itself. Before you sign anything, perform reference checks in your specific sub-vertical. Visit actual sites to see shop-floor data capture and scheduling discipline operating under real production conditions. What looks polished in a demo may behave very differently on a busy shop floor.
Validate Your Choice With a Pilot: Scrap, Downtime, and On-Time Delivery
Execute a proof of value before committing at full scale. Choose a representative production area, run the system under real conditions, and measure results against your pre-implementation baseline. Track OTIF, lead time, scrap and rework rates, schedule adherence, OEE, and downtime. If the system performs, the data will make the ROI case for you.
MES vs ERP: A Side-by-Side Comparison
Still weighing your options? The table below summarizes the key differences across the dimensions that matter most to your operation—from scheduling and data capture to users, reporting, and integration.
| Attribute | MES (Manufacturing Execution System) | ERP (Enterprise Resource Planning) |
| Primary Focus | Real-time shop floor operations, tracking production processes as raw materials transform into finished goods | Managing resources across the entire business: accounting, inventory, sales, human resources |
| ISA-95 Hierarchy Level | Level 3 (between business planning and process control systems) | Level 4 (business planning and logistics) |
| Core Function | Monitors, tracks, documents, and controls the manufacturing process from raw materials to finished products | Creates and manages plant schedules, gathers business information, brings all enterprise facets into one information system |
| Scheduling | Shop-floor job dispatch by individual workstation based on current equipment status and material availability | Material and capacity planning; calculates what materials are needed, quantities, and timing based on sales orders, production orders, inventory levels, and demand forecasts |
| Data Capture Method | Sensors (thousands), barcode scanners, real-time machine signals; captures temperatures, pressures, cycle times, and sensor readings that change second by second | Business transaction data: purchase orders, invoices, inventory movements, and sales orders |
| Quality Management | Process checks, machine process control monitoring, tracks changes through pressures, flows, and torque values; provides part traceability and genealogy of components | Supplier and inventory-level quality records; manages costs and financial reporting |
| Reporting Focus | Overall Equipment Effectiveness (OEE), downtime tracking, real-time defect flags, scrap rates | Purchase suggestions, production schedules, financial reports, costs, cash flow, and orders (spanning hours to months) |
| Primary Users | Operators, process engineers, plant managers | Finance teams, procurement managers, operations executives, sales staff |
| Decision Timeframe | Real-time decisions based on what is happening on the production floor right now | Business planning and operational decisions across the organization |
| Data Sent in Integration | Material consumption, scrap, completion information, resource usage data, order/WIP status, as-built genealogy yields, time events, machine throughput | Production orders, bills of materials, standard operating procedures, change orders, master data, reference product information, production demand |
| Best For | Complex production environments needing real-time machine integration, strict lot/serial genealogy, in-process quality control, or regulatory documentation (FDA, AS9100, IATF 16949) | Finance, purchasing, and order coordination; simple discrete plants with short routings can use ERP’s built-in manufacturing module alone |
| Typical First-Year Investment | Varies depending on integration complexity and hardware requirements | $50,000 for a small cloud deployment to several million dollars for a large, complex enterprise rollout |
Conclusion
The mes vs erp decision doesn’t need to be complicated. Essentially, your choice comes down to where you need the most help right now. ERP works best when you need better coordination across finance, purchasing, and planning. A dedicated mes system makes sense when production complexity, compliance requirements, or real-time control matter most. For many manufacturers, the smartest path forward actually combines both, with mes and erp integration connecting your shop floor to your business operations.
Frequently Asked Questions
MES manages real-time shop-floor activities, including machine performance, production tracking, and process quality. ERP coordinates business-wide functions such as finance, purchasing, inventory, and order planning.
MES serves a different purpose and generally complements ERP rather than replacing it. MES controls production execution, while ERP handles broader business planning and resource management.
Choose an ERP that meets your finance, purchasing, inventory, and production planning needs. Test its scheduling and shop-floor data capture in a pilot, and compare total costs, usability, and vendor support.
Yes. ERP remains useful for coordinating business operations and production plans. Plants with simple production processes may find its built-in manufacturing features sufficient without a separate MES.
Consider a dedicated MES when you need real-time machine integration, detailed lot or serial tracking, in-process quality checks, or regulatory documentation. Integrating it with ERP connects production results to inventory, costing, and business planning.